From raw material
Every transformer moves through twelve controlled stages. Each one has a purpose, an inspection and a record before the next begins.
Manufacturing journey
Twelve stages,
 01Material
Raw Material Inspection
Core metals, winding wire, radiators, bushings and tap changers are received against purchase orders and checked by QA/QC before release to production.
- Matched to ERP purchase order and BOM
- QA/QC acceptance before issue
- Non-conformance reported to vendor via NCR
 02Core
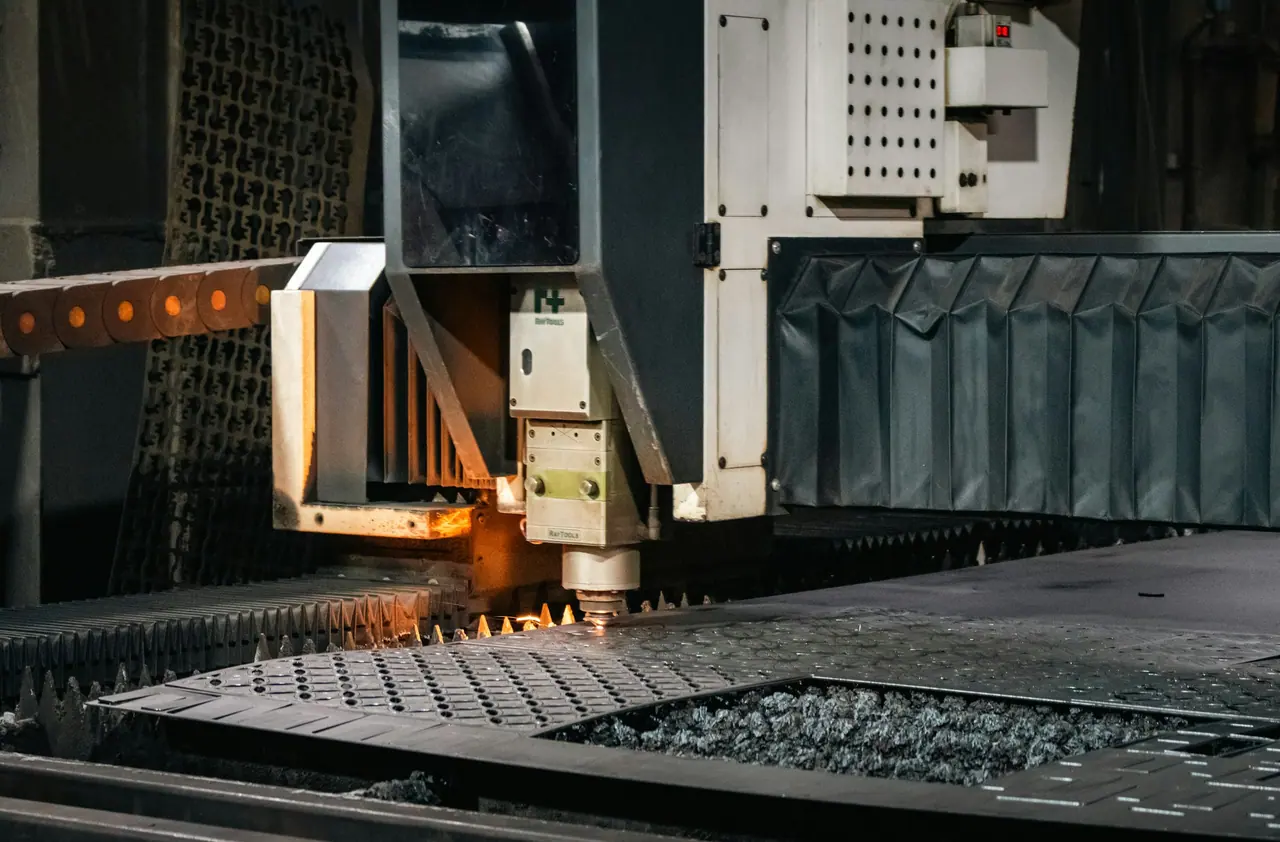
Core Cutting & Lamination
Electrical steel is cut into laminations to the core design, with attention to dimensions and burr — the foundation of low losses.
- Lamination dimensions to drawing
- Edge and burr condition
- Stack sorting by step
- 03Core
Core Assembly
Laminations are stacked into limbs and yokes in a stepped cross-section and secured in the core clamping structure.
- Stack height and step profile
- Joint alignment
- Clamping frame fit
 04Coil
Winding Manufacturing
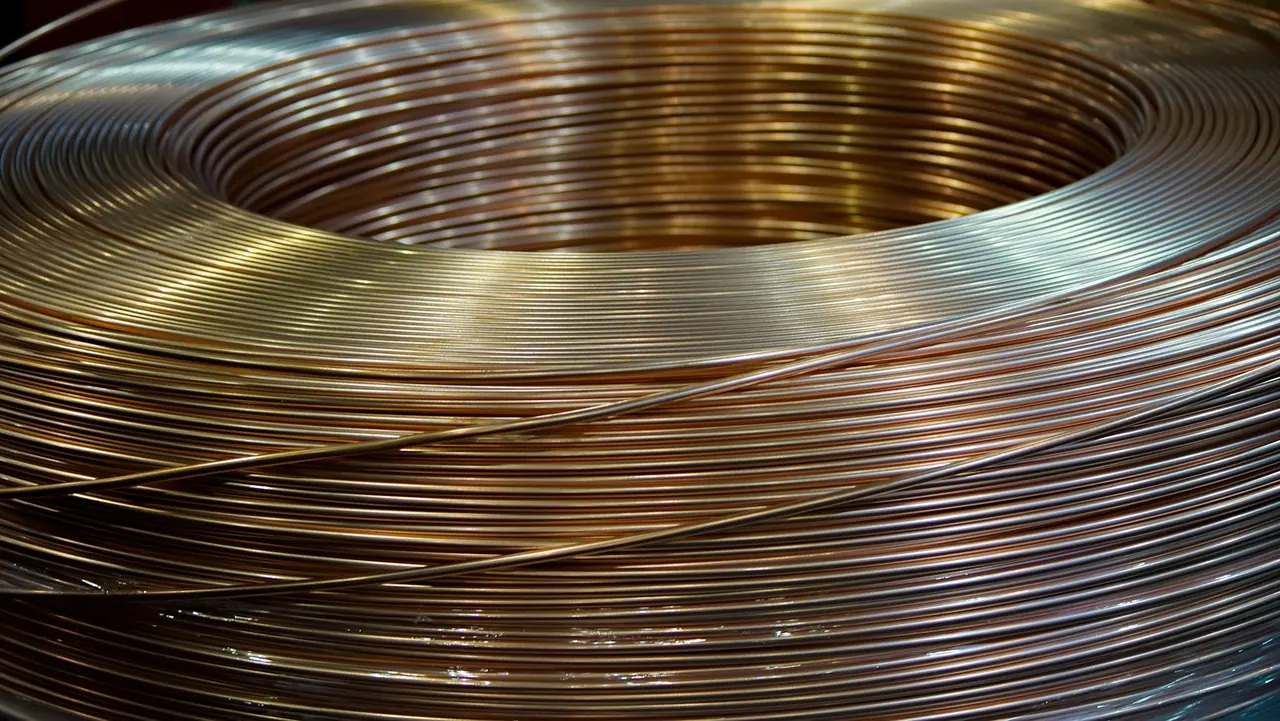
Primary and secondary windings are wound from conductor with insulation, spacers and cooling ducts built in as specified.
- Turns and conductor as per design
- Insulation and duct placement
- Coil dimensions
- 05Coil
Core & Coil Assembly
Windings are lowered over the core limbs, the top yoke is re-stacked and the active part is clamped, braced and connected.
- Concentricity of windings
- Top yoke interleaving
- Lead and tap connections
- 06Tank
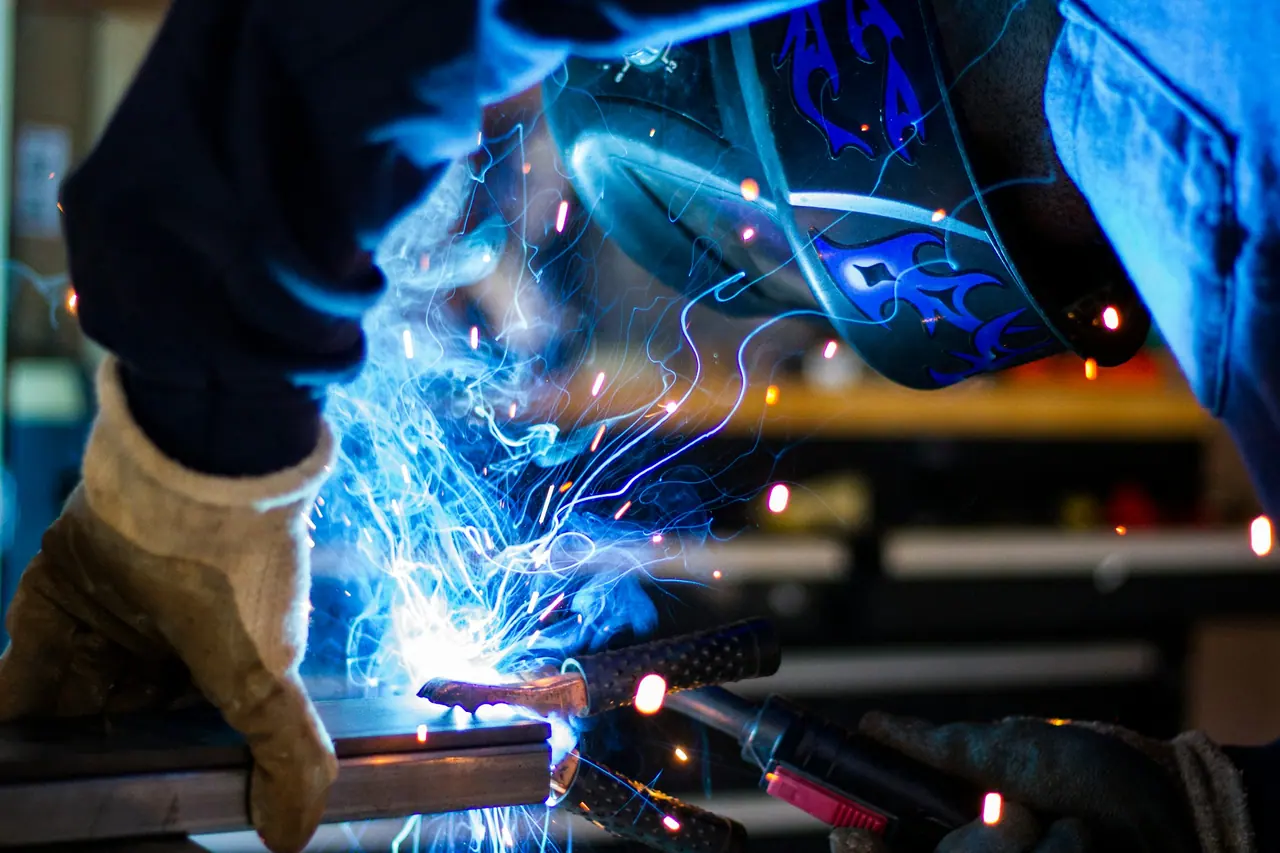
Tank Fabrication
Steel tanks, covers and stiffeners are fabricated and welded, then checked for dimensions and leak-tightness before finishing.
- Weld quality
- Dimensional check
- Leak-tightness before painting
- 07Tank
Tanking Process
The dried active part is lifted by crane and lowered into its tank, positioned and secured.
- Controlled crane lift
- Clearances to tank walls
- Active part locking
- 08Processing
Vacuum & Oil Processing
Moisture is removed from insulation and the tank is filled with treated insulating oil under controlled conditions.
- Insulation dryness
- Oil quality before filling
- Filling under controlled conditions
 09Processing
Final Assembly
Radiators, conservator, bushings, protection devices, indicators and valves are fitted to the customer's accessory specification.
- Accessories to specification
- Gasket and joint tightness
- Wiring and marshalling
 10Verification
Electrical Testing
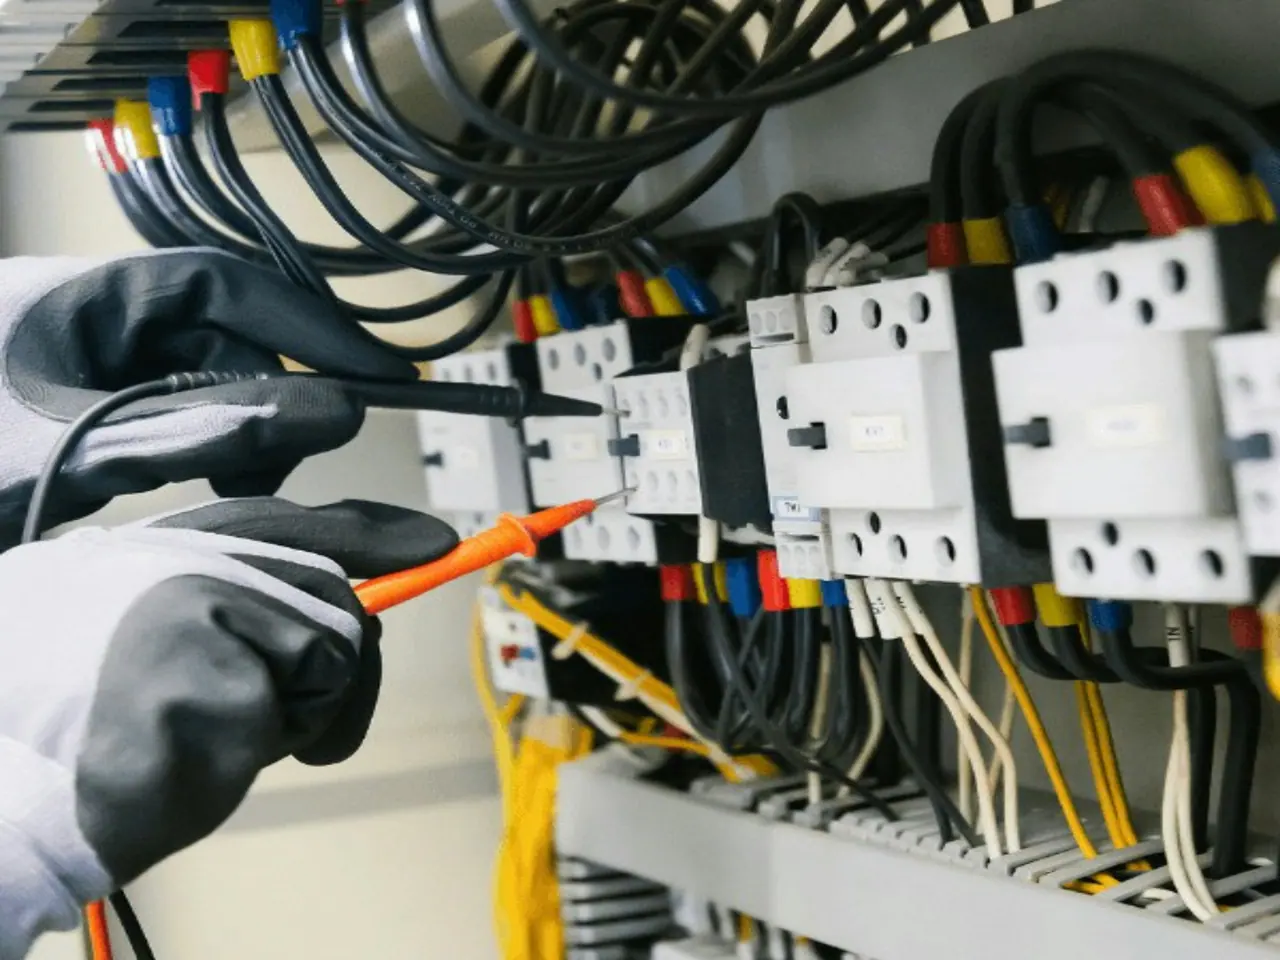
The completed transformer is tested and the results recorded in technical test reports reviewed by the testing function.
- Tests per applicable standard
- Results recorded in test reports
- Review by testing function
 11Verification
Final Quality Inspection
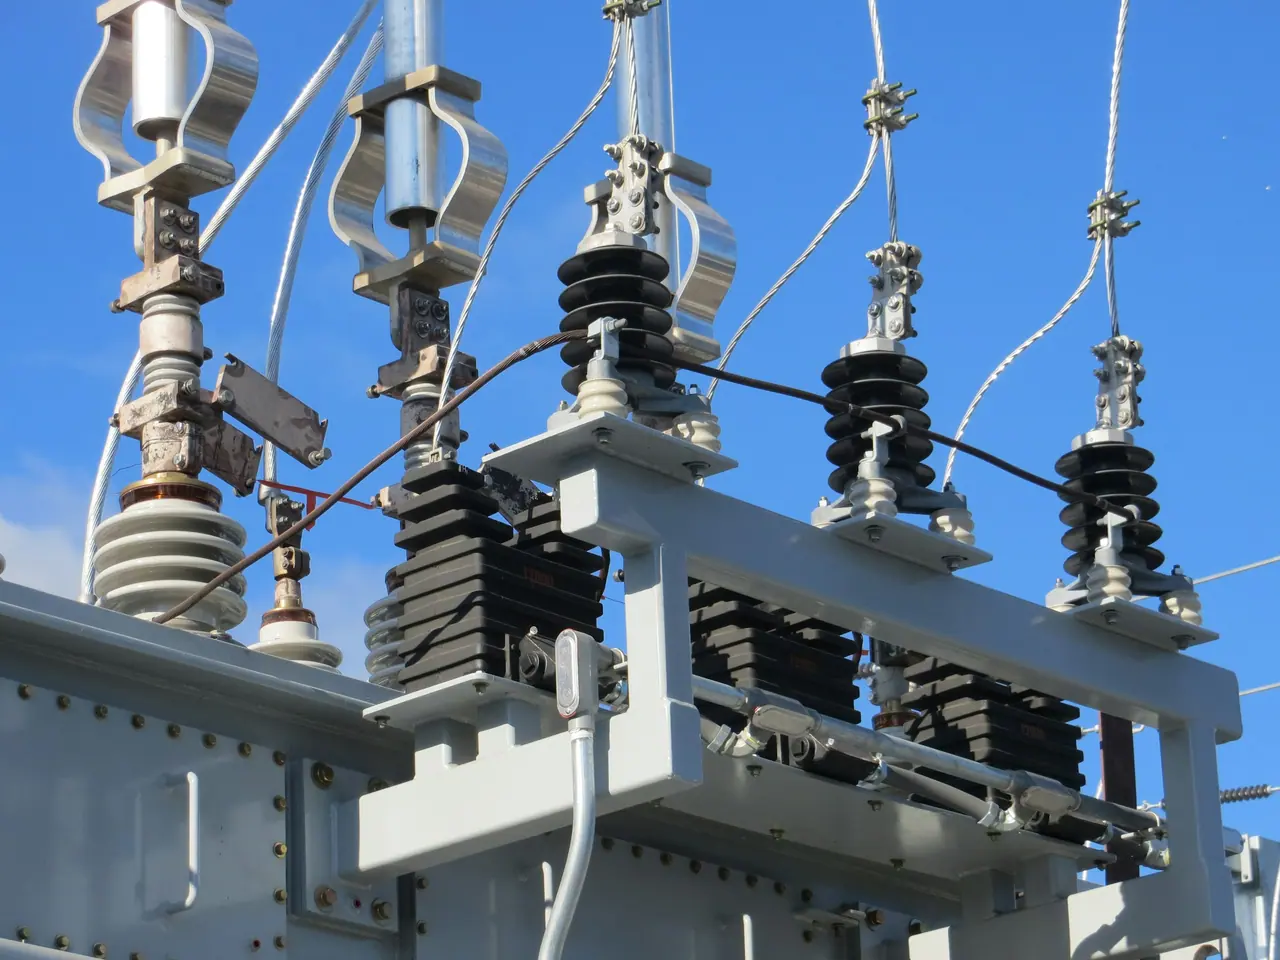
A final inspection confirms finish, fittings, nameplate and documentation — and, where required, customer inspection and dispatch clearance.
- Visual and fitment check
- Documentation complete
- Customer dispatch clearance (MDCC) where applicable
- 12Delivery
Packing & Dispatch
Units are secured on planned trailers or flatbeds with invoices, packing lists, e-way bills, lorry receipts and transit insurance.
- Vehicle planned to load
- Statutory transit documents
- Shipment tracked to delivery
Documented practices
How the process
Drawn from Resonant Equipment's own documented workflow across design, procurement, QA/QC, testing and logistics.
Design-led procurement
Purchase orders are raised in an ERP system against the structural Bill of Materials issued by the design team — so every component traces back to the design.
Approved-vendor sourcing
Core metals, winding wire, radiators, bushings and tap changers are sourced from approved vendors, with quotations reviewed against historical benchmarks.
Non-conformance control
Incoming material is checked by QA/QC. Rejected inputs are handled through formal vendor Non-Conformance Reports (NCR) with replacement or rework.
Test reports before dispatch
Technical test reports are completed and reviewed by the testing function before any finished transformer is booked for dispatch.
Customer dispatch clearance
Where applicable, customer Material Dispatch Clearance (MDCC) is obtained before vehicles are booked — no shipment leaves without clearance.
Heavy-haul logistics
Inbound steel and tanks, and outbound finished transformers, move on planned trailers and flatbeds with full statutory transit documentation.
Get in touch
Let's engineer your next transformer.
Tell us about your application, rating and site conditions. Our team will respond with the next steps.